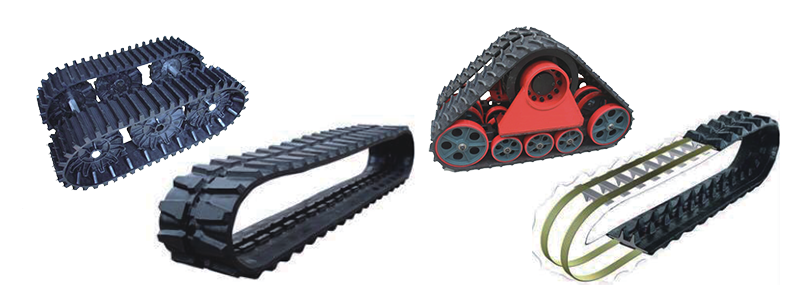
Rubber tracks must retain dimensional accuracy, reinforcement alignment, and dependable bonding after long curing cycles. Variation during loading, tensioning, clamping, heating, or demolding can affect the finished structure. A rubber track vulcanizing machine must therefore maintain a controlled sequence from prepared materials to safe product removal.
The rubber vulcanizing press machine is only one part of this sequence. Process validation should begin with a baseline cure profile, then test temperature distribution, pressure-hold time, steel-cord tension, and handling as an interacting system. A structured trial or DOE should include the largest track and the most demanding approved compound before the operating window is released for production. Stable track production also depends on steel-cord tension, mold condition, thermal distribution, recipe control, and handling. When these elements are managed together, process data becomes more useful and corrective work becomes more precise.
Establish the Baseline Cure Profile
The baseline cure profile should record compound identity, mold and track size, initial material condition, temperature at multiple mold locations, applied pressure, pressure-hold duration, steel-cord tension, and the timing of loading and demolding. Track dimensions, reinforcement position, bonding, surface condition, and cure evidence should be measured after stabilization. This baseline becomes the reference for later parameter trials.
Dekuma links prepared-material feeding to vulcanization and then coordinates demolding and retrieval around the required track cycle. Controlled movement may reduce manual variation around hot, heavy products. Sensors must confirm that the prepared package is positioned correctly before the mold closes.
The handling method must support the uncured assembly without shifting its layers. Gripping points and transfer speed is required to reflect product size and flexibility. A repeatable machine cycle cannot recover structural alignment that was lost during loading.
Incoming checks need to be proportionate to product risk. Compound identity, reinforcement specification, mold readiness, and recipe selection deserve confirmation. Recording these conditions gives engineers evidence when a later inspection result differs from the expected pattern.
Test Temperature, Pressure Hold, and Tension as a System
The rubber vulcanizing press machine works with a constant-tension steel-cord system. Controlled tension supports uniform reinforcement placement and seamless track construction. The target value must be validated for the specific cord, track dimensions, and rubber formulation.
Temperature, pressure-hold time, and steel-cord tension should be tested as an interacting system rather than adjusted separately. A structured trial can use approved high, center, and low settings while keeping material and preparation constant. The response should be evaluated through track dimensions, reinforcement alignment, bonding, surface condition, and cure evidence. The selected window should include operating margin, not merely the single combination that produced the best sample.
Alignment and even force distribution influence thickness and bonding across the long mold. Guides, platens, locking elements, and mold surfaces need scheduled inspection. Gradual wear may first appear as a regional defect rather than an obvious machine alarm.
Mold protection should use controlled movement and reliable position feedback. Residual material or an incorrectly placed component can damage expensive tooling. Automatic closure should proceed to full force only after the closing path is verified.
Validate the Worst-Case Track Size and Compound
Vulcanization combines temperature, pressure, and time to develop the required rubber properties. Long molds can contain thermal differences that a single displayed temperature does not reveal. Distributed checks help identify cold or overheated regions before they affect a large quantity of output.
Sampling should compare positions across the mold and several consecutive cycles rather than relying on one overall average. This separates local heating, pressure, or reinforcement effects from random inspection noise and gives the maintenance team a more precise basis for correcting the process.
Worst-case validation should use the largest approved track, the most demanding compound, and the mold locations that heat most slowly. The study should compare several consecutive cycles after thermal stabilization and record temperature distribution, pressure retention, cure time, tension, and inspection results. A successful average is insufficient if one location remains close to a limit or shows inconsistent bonding.
Recipe storage on the B&R control system helps preserve validated temperature, force, and timing values. Access controls and revision records are important because an undocumented adjustment can create variation that remains hidden until demolding or durability evaluation.
Energy use should be assessed per accepted track. Heating, holding, automatic handling, standby, and auxiliary equipment all contribute. Comparing equivalent products and schedules gives a better indication of performance than one short machine reading.
Lock the Proven Window with Monitoring and Change Control
Once the window is approved, the control plan should define recipe permissions, alarm limits, sampling frequency, trend limits, and restart checks. A compound change, mold repair, heater or sensor replacement, tension-system service, or control-software revision should trigger proportionate revalidation. Production records must connect the track model, material lot, mold, recipe, machine condition, and inspection outcome so that drift can be traced.
Maintenance should cover hydraulics, heating, clamping, tensioning, sensors, loading devices, and demolding systems. Alarm frequency and minor cycle delays may provide earlier warning than a complete failure. Critical spares should be selected according to lead time and effect on production.
Sampling should represent the beginning, middle, and end of a run, as well as different positions along the mold. Track weight, dimensions, surface condition, reinforcement alignment, and cure evidence can reveal localized variation that one final inspection point would miss.
After mold service or compound change, a controlled restart should confirm temperature distribution, tension settings, clamp behavior, and first-off quality. This release step prevents an unverified setup from entering full automatic production and preserves a clear boundary between maintenance and accepted output.
Stable vulcanization results from disciplined control of inputs, reinforcement, force, heat, time, and handling. The press provides the central mechanical conditions, while inspection and maintenance preserve them. This complete approach reduces troubleshooting by showing where variation entered the track-production process. This evidence also supports more reliable future process changes.
Oliver Smith is an experienced blogger at Grammar Globe, Oliver Smith, an expert in English grammar and a master of wit, brings language to life with his playful take on puns. Through his works, he weaves humor into the rules of grammar, making learning fun and engaging for readers of all ages. Discover language with a smile!”